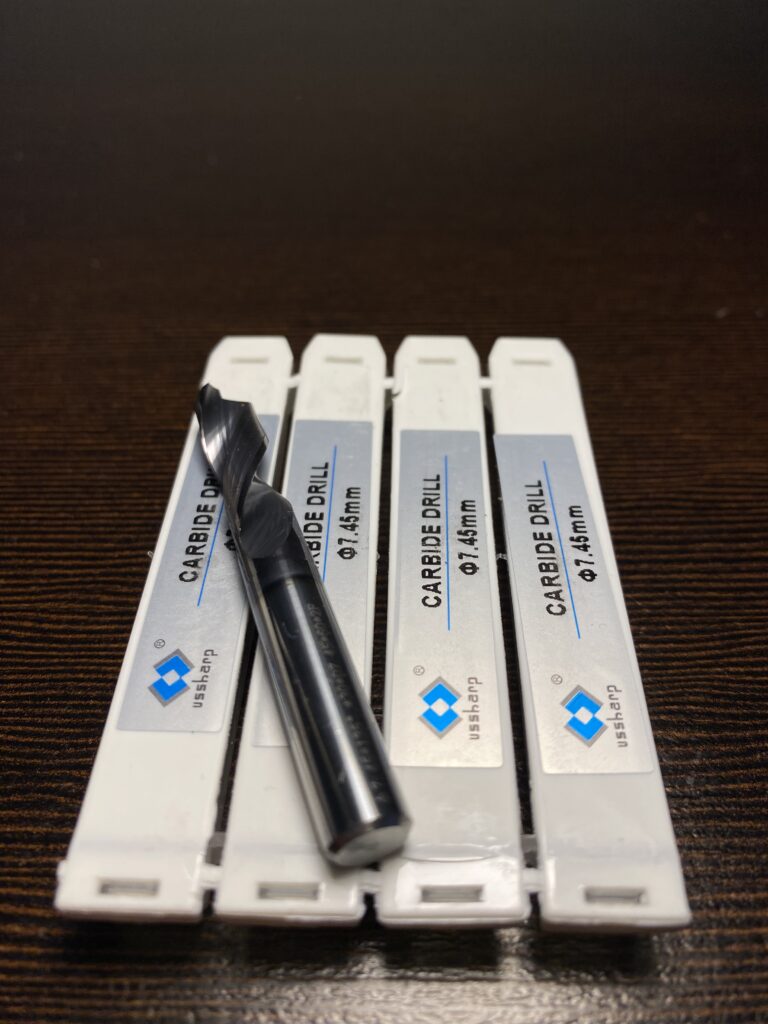
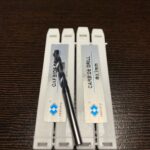
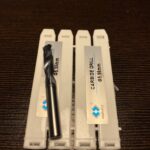
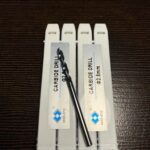
USSHARP Solid Carbide Drills Without Coolant Holes
Zwroty i wymiana →
USSHARP solid carbide drills without coolant holes are a cost-effective choice for accurate CNC drilling with external coolant, mist or air blast. Suitable for steels, stainless steels, cast iron, aluminium alloys and general engineering materials.
| Rozmiar | 1.85, 2.5, 2.8, 3.3, 3.7, 4.2, 4.65, 5.0, 5.55, 6.8, 7.45 |
Description
USSHARP Solid Carbide Drills without coolant holes are straight-shank carbide drilling tools for accurate hole making on CNC machining centres, milling machines and rigid conventional equipment. The solid carbide body gives better stiffness and edge support than standard HSS drills, helping maintain hole position and diameter consistency at carbide cutting speeds. This version has no internal coolant channels, making it a cost-effective choice where external coolant, mist lubrication, compressed air or controlled dry drilling is suitable. It is intended for shallow and medium-depth holes in carbon steel, alloy steel, stainless steel, cast iron, aluminium, copper alloys and engineering plastics. Polished flutes support chip evacuation and reduce chip packing when cutting data and pecking cycles are selected correctly. For best results, use a spot drill or centre drill when positional accuracy is critical, clamp the drill as short as possible and keep runout low. The values below are recommended starting ranges and should be adjusted by diameter, machine rigidity, material condition and coolant method.
Recommended Cutting Data
| Material | Operation | Vc | ap | Feed |
|---|---|---|---|---|
| Carbon and alloy steel | Drilling with external coolant | 60–100 m/min | Full diameter; 1–3×D hole depth | 0.03–0.12 mm/rev |
| Stainless steel | Drilling with external coolant, pecking if required | 35–65 m/min | Full diameter; 1–2.5×D hole depth | 0.02–0.08 mm/rev |
| Cast iron | Dry drilling or air blast | 70–120 m/min | Full diameter; 1–3×D hole depth | 0.04–0.15 mm/rev |
| Aluminium and non-ferrous alloys | High-speed drilling with coolant, mist or air | 120–250 m/min | Full diameter; 1–3×D hole depth | 0.05–0.20 mm/rev |
| Engineering plastics | Drilling with air blast or light coolant | 80–180 m/min | Full diameter; 1–3×D hole depth | 0.04–0.18 mm/rev |
Compatible Tool Holders
- ER precision collet chucks with low runout.
- Hydraulic tool holders for stable CNC drilling.
- Shrink-fit holders for high-speed carbide drilling.
- Precision drill chucks for conventional machines when runout is controlled.
- Straight-shank holders matched to the selected drill shank diameter.
Key Features
- Solid carbide drill design without internal coolant holes.
- Suitable for external coolant, mist lubrication, air blast or controlled dry machining.
- Rigid carbide construction supports accurate hole position and stable diameter control.
- Polished flutes assist chip evacuation in general drilling operations.
- Good price-to-quality option for CNC workshops and maintenance production.
- Best used in rigid setups with short overhang and minimal tool runout.
Suitable Materials
- Carbon steels and alloy steels.
- Stainless steels with suitable coolant and conservative cutting data.
- Cast iron and ductile iron.
- Aluminium and non-ferrous alloys.
- Copper and brass alloys.
- Engineering plastics.
Equivalent or Comparable Inserts
This product is a solid carbide drill, not an indexable insert, so there is no ISO insert code, grade or nose radius to match. Comparable general-purpose solid carbide drill families are available from brands such as Guhring, Sandvik Coromant, Kennametal, YG-1 and Dormer Pramet. Always verify drill diameter, flute length, shank diameter, point geometry and coolant-hole requirement before substitution.