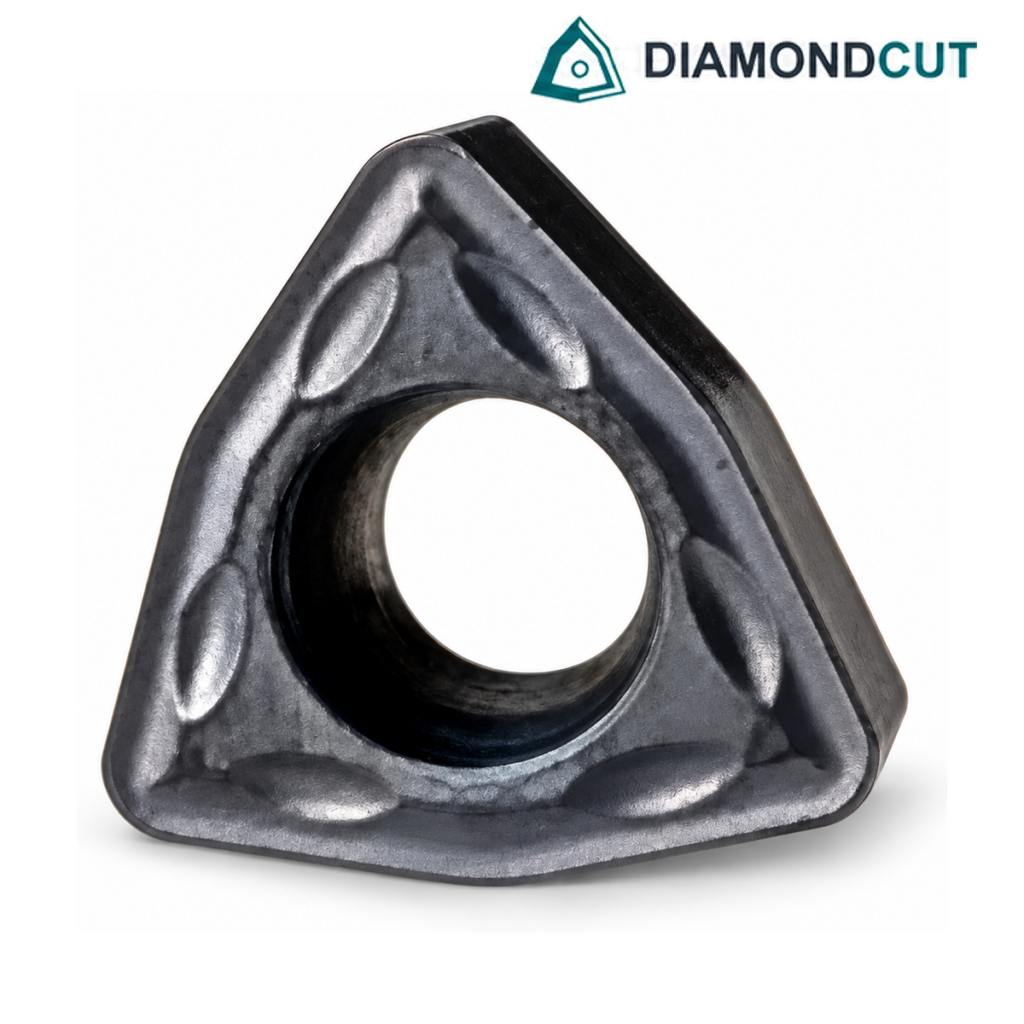
WCMT 040208FN OS9101P Drilling Insert
Palautukset ja vaihdot →
Description
The WCMT 040208FN OS9101P is a trigon-style indexable insert widely used in U-drills and other indexable drilling systems where edge strength and predictable wear matter most. Built around a PVD-coated surface and a versatile application window, it supports mixed-material production across steels, stainless steels, and cast irons. Choose the WCMT 040208FN OS9101P when you want stable hole-making results with a practical speed range and good resistance to flank wear in everyday machining. In drilling, this grade family is intended for materials up to HRC <45 and is typically run within Vc 80–180 m/min, depending on workpiece group and setup rigidity. If you need a dependable insert for indexable drilling that stays consistent across common shop materials, the WCMT 040208FN OS9101P is a reliable option for standard production and job-shop work.
updated Speed carbide inserts G…
Code Breakdown
-
W = trigon insert shape (80°)
-
C = clearance angle class “C”
-
M = tolerance class “M”
-
T = ISO clamping/hole style “T”
-
040208 = ISO size/thickness/radius code (the “08” commonly indicates 0.8 mm nose radius)
-
FN = maker’s chipbreaker / edge-prep geometry code
-
OS9101P = supplier grade in the OS9101 drilling family (ISO P20–P30 / M20–M30 / K20–K30, PVD, black, HRC <45, Vc 80–180)
updated Speed carbide inserts G…
Key Features
-
Universal ISO range for steel, stainless, and cast iron applications
updated Speed carbide inserts G…
-
PVD-coated, black finish for wear resistance in hole-making
updated Speed carbide inserts G…
-
Intended for indexable drilling tools (U-drills) with stable cutting conditions
-
Practical cutting-speed window for consistent production drilling
updated Speed carbide inserts G…
Equivalent (Sandvik, Seco, Kennametal, Iscar)
Select the WCMT 040208 insert size in each brand’s indexable drilling range, then match the closest chipformer/edge prep to “FN” based on your toolmaker’s recommendation.
Recommended Cutting Data / Application
-
Operation: indexable drilling (U-drills), through holes and pre-drilled entry preferred
-
Material groups: ISO P/M/K (P20–30, M20–30, K20–30)
updated Speed carbide inserts G…
-
Vc: 80–180 m/min (start lower for stainless/cast iron; raise for steels if stable)
updated Speed carbide inserts G…
-
Use coolant where possible; reduce speed for unstable clamping or interrupted entry.